Engineered for commercial kitchens, hospitality chains, and industrial food service operations. Featuring heavy-gauge SUS304 stainless steel, precision temperature control, and leak-proof hermetic seals.
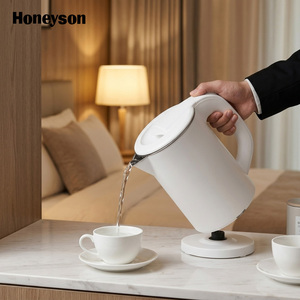
Compact food-grade 304 stainless steel thermal kettle designed for room service, boutique hospitality, and mobile beverage operations. Vacuum-insulated double-wall body prevents exterior heat transfer while preserving liquid temperature.
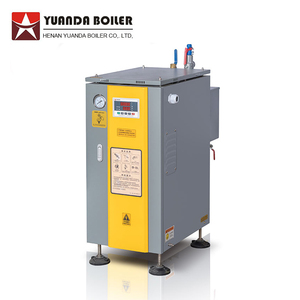
Commercial-scale continuous liquid boiling and storage unit engineered with high-yield 120 kW heating elements. Designed for centralized food processing plants, large-scale catering facilities, and institutional kitchens.
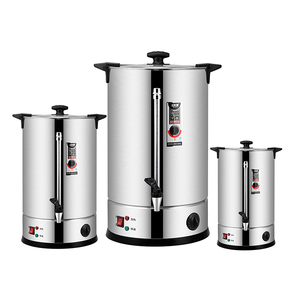
CE-certified 15-liter capacity catering urn built from heavy-duty 304 austenitic stainless steel. Features dual-stage precision thermostat control, anti-scald handles, and a high-flow commercial dispense valve.
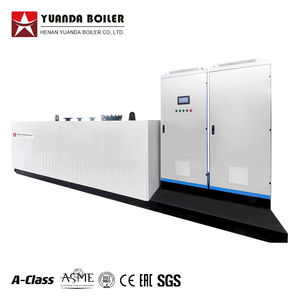
Factory-direct commercial water heating boiler with integrated expansion tank and dual-circuit fluid loops. Built to strict ISO/CE standards for hotel central kitchens, sanitization stations, and facility heating.
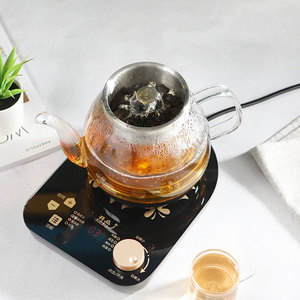
Hybrid borosilicate glass and SUS304 stainless steel infusion storage kettle. Includes removable fine-mesh steaming rack and filter basket for commercial tea houses, coffee bars, and executive hospitality suites.
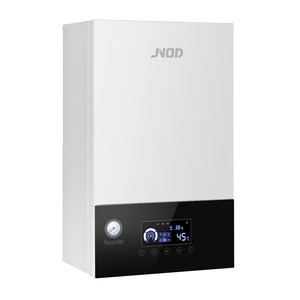
Space-saving wall-mounted electric boiler unit equipped with micro-computer temperature regulators. Engineered for commercial sanitation, dishwashing prep sinks, and compact restaurant setups.
High-efficiency commercial liquid boiler constructed with a durable heat-resistant outer shell and food-grade stainless steel internal chamber. Features a clear volume monitoring sight glass and automatic auto-shutoff safety sensors.
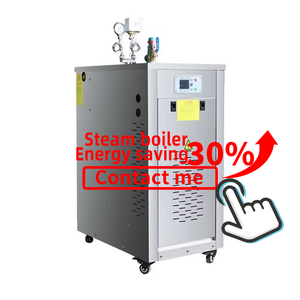
Advanced vertical double-circuit commercial heating boiler designed for simultaneous hot water supply and steam distribution in high-volume hospitality, restaurant, and processing plant applications.
Established in 1974 by Shri J. Bhawarlal Bohara, BOHARA Group has grown into an international powerhouse in premium stainless steel cookware, insulated food hotpots, storage canisters, and commercial catering equipment.
Under the visionary leadership of Managing Director Mr. Rakesh Bohara and the technological innovations introduced by Mr. Vijayraj Bohara, BOHARA Group operates with an unwavering commitment to sincerity, engineering precision, and customer-first service. Our global distribution headquarters in Dubai (BOHARA TRADING CO LLC) serves as a strategic sourcing node connecting commercial buyers across Europe, the Middle East, Asia, and the Americas.
Every stainless steel food storage canister, insulated hotpot, and commercial boiler manufactured in our facilities undergoes rigorous automated defect screening, pressure testing, and chemical passivation. We adhere to FDA 21 CFR, EU 1935/2004, LFGB, and ISO 9001:2015 standards to ensure absolute food safety, zero heavy-metal leaching, and high tensile resistance against mechanical stress.
An authoritative technical breakdown for corporate procurement managers, quality assurance specialists, and commercial importers evaluating industrial food storage hardware.
Selecting the appropriate alloy is the foundation of long-term canister durability. Standard food containers often utilize low-nickel 201-grade steel, which is prone to pitting corrosion in saline environments. Professional-grade canisters engineered by BOHARA strictly implement Austenitic Stainless Steel Grade 304 (18/8 Chromium-Nickel matrix) or Grade 316L (containing 2-3% Molybdenum) for acidic ingredient storage.
Key Metallurgical Metric: PREN (Pitting Resistance Equivalent Number) > 19.0 for SUS304, ensuring complete immunity to organic food acids and commercial cleaning chemicals.
Structural failure in food storage vessels typically occurs at welded seam joints. BOHARA utilizes single-piece hydraulic deep-drawing techniques that transform heavy-gauge metal sheets into seamless cylindrical canister bodies without structural weak points. Following mechanical forming, canisters undergo Electro-Chemical Passivation to build an oxide micro-barrier layer (Cr2O3), eliminating microscopic pores where bacteria propagate.
Maintaining air-tight and liquid-tight closure requires precise seal engineering. BOHARA canisters integrate dual-injection food-grade silicone gaskets certified under FDA 21 CFR 177.2600. Combined with ergonomic heavy-duty stainless steel latch clamps or precision-machined screw lids with built-in steam release valves, these canisters prevent volatile aromatic degradation and atmospheric moisture ingress.
How evolving environmental regulations, commercial automation, and material science are reshaping the stainless steel container and catering ware landscape.
Global legislative frameworks, such as the EU Single-Use Plastics Directive and stringent corporate ESG metrics, are forcing major hospitality chains, airlines, and commercial food processors to eliminate polycarbonate and plastic storage containers. Stainless steel food canisters offer a 100% recyclable, non-degrading solution with an operational lifespan exceeding 15 years, drastically reducing Total Cost of Ownership (TCO) for enterprise buyers.
Modern commercial logistics require real-time visibility over cold-chain storage and shelf-life integrity. Next-generation canister procurement is shifting toward smart containers equipped with internal micro-vacuum pumps, digital temperature displays, and RFID tracking tags. These systems provide automated logging of ingredient freshness, HACCP compliance tracking, and automated inventory management for commercial kitchens.
Beyond traditional mirror polishing, advanced manufacturing facilities are applying ion-beam physical vapor deposition (PVD) and silver-nanoparticle coatings to stainless steel interiors. This technology actively inhibits microbial biofilm formation, reducing bacterial cross-contamination risks in commercial bulk food storage by up to 99.99%.
Global trade volatility has made long-distance lead times unpredictable. Enterprise procurement directors are prioritizing manufacturers with localized hub warehousing. BOHARA Group’s extensive distribution network in Dubai, UAE, acts as a seamless transit node, allowing fast 7-to-14 day dispatch to European, Middle Eastern, and African commercial ports.
A detailed comparative audit of BOHARA commercial canisters against standard market options, highlighting technical standards and verification methodologies.
| Performance & Material Attribute | Standard Commercial Canister | BOHARA Heavy-Duty Canister | Testing Standard & Verification |
|---|---|---|---|
| Raw Material Composition | Recycled 201 Stainless Steel (High Manganese) | Virgin SUS304 / SUS316 Austenitic Steel | Spectrometric Chemical Alloy Analysis |
| Wall Thickness Uniformity | 0.3mm - 0.4mm (Vulnerable to denting) | 0.6mm - 1.2mm Heavy-Gauge Deep Drawn | Ultrasonic Thickness Gauge Testing |
| Hermetic Seal Standard | Standard PVC / Rubber Gasket | Food-Grade Platinum-Cured Silicone | FDA 21 CFR 177.2600 & LFGB Compliance |
| Corrosion Resistance (Salt Spray) | Rusting observed at 24 - 48 Hours | No oxidation at 500+ Hours Continuous Spray | ASTM B117 Neutral Salt Spray Test |
| Surface Finish & Passivation | Basic Mechanical Polishing | Electro-Polished (Ra < 0.4 µm) + Passivated | Surface Roughness Profilometer Test |
| Thermal Shock Resistance | Deforms under sudden delta T (50°C) | Stable across Delta T (-40°C to +250°C) | Thermal Cycling Stress Audit |
Direct technical responses addressing common inquiries from hotel purchasing teams, wholesale distributors, and OEM buyers.
SUS304 contains a minimum of 18% Chromium and 8% Nickel, establishing a stable austenitic crystalline structure that prevents corrosion, rusting, and chemical leaching when exposed to acidic food products (such as tomato sauces, vinegars, and citrus dressings). Lower-cost alternatives frequently utilize 201-series steel, which substitutes manganese for nickel, leading to surface oxidation, metallic taste transfer, and premature structural failure in commercial kitchens.
Yes. BOHARA Group provides comprehensive OEM/ODM services. We offer custom deep-drawing mold manufacturing, laser-engraved corporate logos, custom color finishes (PVD gold, rose gold, matte black), specialized latch systems, and tailored retail packaging tailored to client specifications.
All BOHARA food storage canisters and commercial catering equipment comply with key international safety benchmarks, including US FDA 21 CFR 175.300, European Union EU Regulation No 1935/2004, German LFGB standards, and CE certification for all electrical thermal boiler systems.
Our hermetic canisters feature precision-molded, food-grade silicone gaskets seated within a recessed lid channel. When the heavy-duty stainless steel side latches are engaged, uniform downward compression is applied across the entire rim perimeter, creating a airtight seal that blocks moisture, air, and pest infiltration.
Standard catalog items maintained at our Dubai distribution hub feature flexible MOQs starting at 100 units per SKU. For fully customized OEM orders involving specialized tooling, standard MOQs range from 500 to 1,000 units. Lead times average 15 to 30 business days depending on order complexity and destination port.
Yes. The non-porous SUS304/SUS316 body and removable silicone gaskets are fully heat-resistant and capable of withstanding standard industrial dishwashers, high-pressure steam sanitation cycles, and thermal sterilization up to 250°C without warping or degrading.
Direct factory pricing, custom OEM tooling, certified food-grade materials, and rapid international fulfillment from BOHARA Group. Request a technical quote or custom product catalog today.
Contact Us