Engineered with high-grade SUS304/SUS316 stainless steel, heavy-duty vacuum insulation, and ergonomic pour spouts. Direct factory supply for wholesale and commercial buyers worldwide.
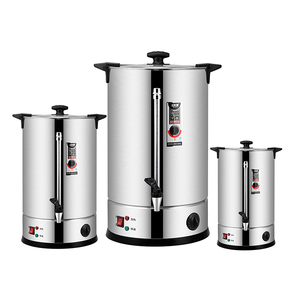
Technical insight into metallurgy, vacuum thermal dynamics, and commercial foodservice ergonomics from China's leading OEM exporter.
Our stainless steel insulated beverage pitchers utilize premium SUS304 (18/8) and optional medical-grade SUS316 stainless steel. This guarantees complete resistance against pit corrosion caused by acidic beverages like coffee, tea, fruit juices, and dairy compounds. High nickel and chromium ratios prevent metallic leaching and maintain chemical neutrality across extreme temperature ranges.
Using automated high-vacuum annealing furnaces operating at temperatures exceeding 1000°C, air is evacuated between the double-steel walls to less than 10⁻³ Pa. An internal copper coating layer reflects infrared radiation, reducing heat loss via conduction, convection, and radiation. Liquids remain boiling hot (>75°C) for 12 hours or ice-cold (<5°C) for 24 hours.
Designed specifically for high-volume commercial dining environments, our pitchers incorporate fluid dynamic spouts engineered to eliminate drips and splashback. Push-button vacuum lever lids feature food-grade silicone gaskets certified under FDA 21 CFR and LFGB standards, ensuring leak-tight transportation for room service and outdoor catering operations.
Comparative benchmarking of vacuum-insulated pitchers for wholesale procurement decision-making.
| Parameter / Feature | Commercial Stainless Steel Vacuum Pitcher | Standard Single-Wall SS Pitcher | Glass-Lined Thermal Carafe |
|---|---|---|---|
| Thermal Retention (Hot) | > 78°C @ 6 hrs / > 65°C @ 12 hrs | < 40°C @ 1 hr (Rapid Dissipation) | > 70°C @ 6 hrs |
| Impact & Shatter Resistance | Ultra-High (Heavy-Duty Commercial Grade) | High (Prone to Denting) | Low (High Risk of Glass Implosion) |
| Material Safety Certification | FDA, LFGB, RoHS, DGCCRF Compliant | Standard Metallic Grade | Fragile Internal Component Risk |
| Outer Body Surface Temp | Cool-Touch Touchpoint (Safety Safe) | Scalding Danger (>85°C) | Moderate Cool-Touch |
| B2B Service Life & ROI | 10+ Years (Zero Maintenance Core) | 2-3 Years | 1-2 Years (Frequent Liner Replacement) |
Founded by Shri J. Bhawarlal Bohara and expanded globally under the leadership of Managing Director Mr. Rakesh Bohara, the BOHARA Group stands as an international beacon of quality in stainless steel houseware, tableware, cookware, and commercial catering ware.
Operating from high-capacity manufacturing centers and global distribution hubs in Dubai (BOHARA TRADING CO LLC), we service institutional buyers, hospitality chains, and B2B distributors in over 50 countries. Our state-of-the-art facilities feature hydraulic deep-drawing presses, automated robotic laser welders, electrochemical polishing units, and rigorous multi-stage quality assurance labs.
Key technological transformations shaping global wholesale sourcing strategies for insulated pitchers and catering kettles over the next decade.
Commercial buyers are prioritizing insulated pitchers equipped with digital micro-LED lids and wireless IoT sensors. These systems allow waitstaff and banquet managers to verify beverage temperatures instantly without opening seals, preventing thermal leakage and ensuring regulatory temperature compliance for dairy-based beverages.
Environmental directives and stringent consumer safety standards are pushing commercial procurement towards 100% plastic-free hot water contact paths. Next-generation insulated beverage pitchers feature full stainless steel spouts, laser-welded interior stoppers, and medical-grade platinum-cured silicone seals to guarantee zero microplastic migration.
Physical Vapor Deposition (PVD) gold, matte black, titanium, and champagne rose finishes are replacing traditional electroplating. PVD offers extreme surface hardness, fingerprint resistance, and superior dishwasher tolerance, matching modern hotel interior design themes while maintaining commercial durability.
To reduce total cost of ownership (TCO) in hotel operations, modern insulated pitchers feature modular disassemblable pour valves, quick-change silicone seal rings, and standard-fit replacement handles. Institutional buyers can perform routine servicing in-house, significantly extending product longevity.
Macroeconomic factors driving commercial growth and volume demand across key regional markets.
The global commercial beverage pitcher market is undergoing substantial growth, driven by expanding luxury hotel chains, institutional catering contracts, corporate dining facilities, and eco-friendly hospitality initiatives replacing single-use plastic bottles with reusable vacuum carafes.
Middle East & North Africa (MENA): Driven by massive investments in luxury tourism and corporate infrastructure, high demand exists for premium gold-accented thermos pitchers, traditional Arabic Dallah thermal pots, and high-capacity banquet water boilers.
North America & Europe: Procurement is centered on stringent compliance certification (NSF, FDA, LFGB), dishwasher-safe commercial thermal pitchers, and heavy-gauge stainless steel vacuum carafes tailored for executive coffee breaks and healthcare food service.
Essential answers for corporate buyers, wholesale importers, OEM partners, and procurement directors.
We manufacture primarily using high-grade food-safe SUS304 (18/8 Stainless Steel) for both internal liners and outer shells. For specialized marine catering, medical institutions, or high-salinity environment applications, we provide optional SUS316 (18/10 Stainless Steel) inner liners, providing elevated molybdenum content for exceptional resistance to severe chemical pitting and chloride corrosion.
Every production batch undergoes automated computerized 100% vacuum temperature testing. Pitchers pass through a multi-stage thermal chamber inspection where performance is logged over 6 and 12-hour intervals. Units falling outside strict temperature retention parameters (>75°C at 6 hours for boiling water) are automatically rejected by robotic sensors on the assembly line.
Our products are manufactured under strict ISO 9001:2015 quality management systems. All beverage contact components—including stainless steel bodies, silicone sealing rings, and BPA-free polypropylene lids—are tested and certified compliant with U.S. FDA 21 CFR 177.1210, European LFGB, European Union CE directives, and French DGCCRF standards.
Standard catalog models are available with flexible minimum order quantities starting at 500 units per SKU. Custom OEM orders featuring bespoke body colors (PVD gold, matte finish, custom pantone lacquers), private label laser engraving, or custom retail packaging typically require an MOQ of 1,000 to 3,000 units depending on technical specifications. Standard mass production lead times range from 25 to 35 days after artwork approval.
Yes. Our double-wall SUS304 and SUS316 stainless steel interiors feature electropolished, non-porous passivation layers that resist acid corrosion from citrus juices, iced tea, coffee, and carbonated beverages. Furthermore, our pressure-relieving lid valves allow safe release of minor gas build-up without compromise to vacuum tightness.
We provide comprehensive export logistics support including FOB China/Dubai, CIF destination port, and DDP solutions worldwide. All shipments are protected with high-density drop-tested B2B mail-order packaging. In the rare event of manufacturing defects, Bohara Group provides a 1-year commercial warranty with immediate replacement or credit adjustment on subsequent orders.
Connect directly with our engineering and export team for technical catalogs, factory-direct wholesale pricing, custom OEM quotes, and sample evaluations.
Inquire Now