Directly sourced from our precision manufacturing lines. Every unit is engineered for optimal thermal efficiency, high tensile strength, and rigorous commercial kitchen compliance.
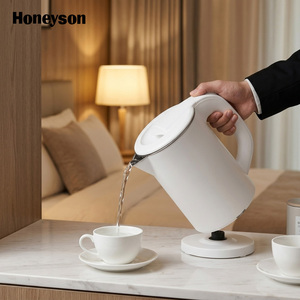
Precision double-wall thermal insulation with 304 food-grade inner pot. Ideal for commercial hospitality and hotel suites.
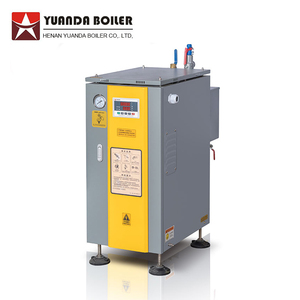
High-capacity heavy-duty stainless steel pressure-tested boiler designed for continuous commercial & catering water heating.
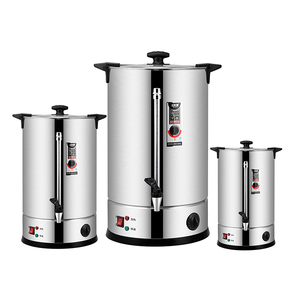
CE-certified high-volume catering boiler crafted from premium 18/8 stainless steel with automatic anti-dry protection.
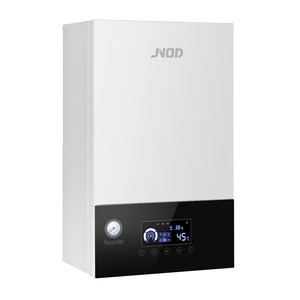
Custom engineered dual-circuit central heating electric boiler constructed with thick-gauge anti-corrosive steel shells.
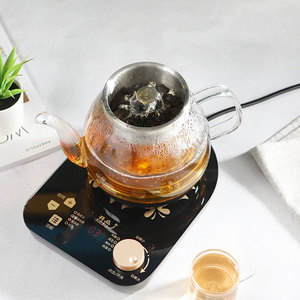
High borosilicate thermal glass base coupled with 304 stainless steel filter tank for tea, coffee, and specialty brewing.
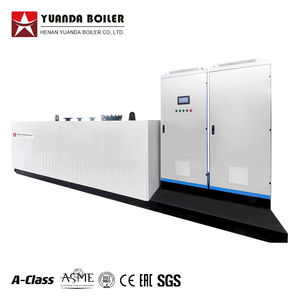
Space-saving commercial hydronic boiler with intelligent micro-processor control and micro-welded stainless water tubes.
High-efficiency boil-dry protected catering kettle featuring clear level gauge and food-safe inner stainless floor plate.
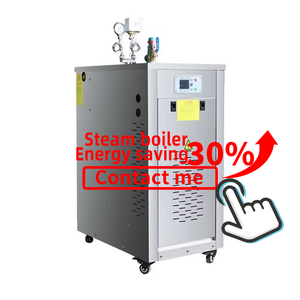
CE-marked commercial multi-circuit boiler unit optimized for heavy restaurant operations, hot water delivery, and steam generation.
An authoritative analysis of alloy selection, ply encapsulation, thermal distribution vectors, and structural warping defense for high-turnover foodservice operations.
Commercial heavy-duty frying pans must withstand extreme salt concentrations, acid exposure (tomato/citrus reductions), and thermal shocks up to 450°C. Standard culinary cookware relies on AISI 304 (18/8 Chrome-Nickel), providing high tensile strength and oxidation resistance. However, for elite commercial environments, our custom OEM lines utilize **AISI 316L (18/10/2 Mo)**, fortified with Molybdenum to prevent pitting corrosion under high-temperature saline cooking processes.
Stainless steel possesses lower thermal conductivity ($16 \text{ W/m}\cdot\text{K}$) compared to pure aluminum ($237 \text{ W/m}\cdot\text{K}$). To overcome hot-spotting, BOHARA utilizes **Tri-Ply and 5-Ply Cladding Technologies**. A 1050/3003 commercial aluminum core is cold-rolled under 800 metric tons of pressure between inner food-grade 304 stainless steel and an outer magnetic 430 stainless steel layer, delivering edge-to-edge heat uniformity in under 90 seconds.
Thermal stress causing bottom bowing ("oil-camber warping") is a primary failure mode in institutional cookware. Our OEM frying pan bases feature a precision concave cold-compensation offset (0.4mm inward curve at ambient temperature). When subjected to high BTU gas burners or 5kW induction surfaces, the thermal expansion vectors align perfectly flat, ensuring 100% surface contact with zero energy dissipation.
| Engineering Attribute | Standard Single-Ply SS Pan | BOHARA Heavy Duty Tri-Ply OEM | BOHARA 5-Ply Commercial Skillet |
|---|---|---|---|
| Layer Configuration | Single Layer SS 201 / 304 | 304 SS + Pure Al + 430 SS | 304 SS + Al Alloy + Pure Al + Al Alloy + 430 SS |
| Wall Thickness Range | 0.8mm – 1.2mm | 2.5mm – 3.5mm Heavy Gauge | 3.8mm – 4.5mm Ultra Heavy Duty |
| Heat Distribution Speed | Uneven (Prone to hot spots) | Rapid & Uniform (Edge-to-Edge) | Maximum Thermal Retention & Response |
| Induction Compatibility | Optional (Requires disk bottom) | 100% Integrated Magnetic Base | 100% High-Efficiency Induction Core |
| Handle Fixing Stress Limit | Spot Welded (Low Impact) | Heavy Riveted (3x Solid SS Rivets) | Dual-Fixing (Cast SS Weld + Solid Rivets) |
| Warping Resistance Rating | Moderate (< 200°C shock) | Extreme (< 400°C heat shocks) | Maximum Industrial Grade (< 500°C continuous) |
How regulatory evolution, commercial induction migration, and non-stick safety standards are reshaping institutional pan manufacturing.
European Union REACH updates and US FDA mandates are strictly banning fluoropolymer-based non-stick surfaces (PTFE/PFAS) in commercial environments due to persistent bio-accumulation. The procurement trajectory is shifting decisively toward **Sol-Gel Ceramic non-stick, Plasma Titanium Nitride (TiN) ion plating**, and high-polish mechanical micro-embossed stainless surfaces requiring zero chemical coatings.
Commercial kitchens are rapidly decoupling from fossil gas ranges to cut ventilation energy loads and comply with corporate net-zero carbon goals. Procurement specifications now mandate full-aperture magnetic friction-welded bases or full tri-ply bodies that deliver instant magnetic resonance on commercial induction ranges without thermal humming or efficiency drop-offs.
Global importers and hotel chains are moving away from single-source manufacturing risks. Partners with strategic export logistics hubs—such as **BOHARA Group’s extensive footprint in Dubai, UAE** combined with agile manufacturing facilities—allow buyers to maintain safety stock buffers, lower tariff exposure, and achieve shorter shipping lead times to EMEA and Americas.
From 3D CAD modeling and prototype stamping to PVD surface coating and laser branding, our industrial setup is tailored for high-volume custom orders.
Engineering custom pan diameters, depth, lip flare angles, and weight distribution according to precise client specification sheets.
Forming heavy-gauge stainless metal discs under 1,000-ton hydraulic presses to guarantee uniform structural wall thickness.
Robotic TIG welding or heavy-duty triple rivet insertion for ergonomically balanced, cool-touch cast stainless handles.
Mirror polishing, satin brush, PVD Gold accents, fiber-laser logo etch, and ISO 9227 salt spray anti-corrosion testing.
Founded in 1974 by Shri J. Bhawarlal Bohara, the BOHARA Group has grown from a visionary cookware enterprise into an international houseware and commercial catering manufacturing powerhouse. Operating under the strategic direction of Managing Director Mr. Rakesh Bohara and international expansion led by Mr. Vijayraj Bohara, our group serves wholesale distributors, hotel chains, and retail brands across 50+ countries.
Our core pillar has remained unchanged for half a century: combining uncompromised raw material selection with continuous engineering innovation to produce kitchenware built for lifetimes of performance.
Addressing critical engineering, material composition, MOQ, and private labeling inquiries for commercial sourcing managers.
For commercial foodservice environments exposed to high salinity and heavy acidic cooking, AISI 304 (18/8) is the industry standard for interior pan surfaces, while AISI 316L (18/10/2 Mo) offers superior pitting resistance. The exterior base layer should utilize magnetic AISI 430 (18/0) steel to ensure maximum energy transfer on commercial induction cooktops.
Single-ply stainless steel has poor thermal conductivity, causing concentrated heat spots that scorch food and warp the pan floor. Tri-Ply or 5-Ply clad construction encapsulates high-purity aluminum alloys between stainless layers. Aluminum transfers heat horizontally 15 times faster than steel, eliminating hot spots and keeping the cooking surface thermally uniform across all burner types.
Our standard OEM production MOQ starts at 500 units per pan size for standardized tooling configurations with laser logo etching. For fully custom mold development (unique lip angles, custom handle castings, or specialized multi-ply wall thicknesses), typical MOQs range from 1,000 to 2,000 units depending on raw sheet tonnage requirements.
Yes. All BOHARA commercial frying pans feature either a full tri-ply continuous clad bottom or an impact-bonded magnetic stainless steel disc (capsule bottom) applied under 2,500 tons of friction pressure. This prevents bottom delamination and guarantees rapid magnetic flux coupling on high-power (3.5kW to 5kW) induction hobs.
Heavy-duty solid stainless steel rivets (3-point installation) offer maximum mechanical shear strength for high-volume pans subjected to constant shaking, flipping, and heavy food loads. For maximum hygiene in sterile commercial environments, we also offer high-frequency micro-welded handles that eliminate internal pan rivet heads for effortless cleaning.
In compliance with global anti-PFAS regulations, we manufacture pans using 100% PFOA/PFAS-free Sol-Gel Ceramic coatings, multi-layer reinforced granite mineral coats, and high-temp Titanium Nitride (TiN) surfaces. We also supply raw, un-coated satin-brushed interior pans designed for natural oil seasoning.
Our production batches are thoroughly tested and certified under FDA 21 CFR, German LFGB, EU Directive 1935/2004, ISO 9001:2015, and CE standards. Full material test certificates (MTC) detailing steel chemical composition and heavy metal migration analysis are provided prior to shipment dispatch.
Pre-production sample verification typically takes 7 to 12 days. Once sample approval and deposit confirmation are established, mass manufacturing lead time is approximately 30 to 40 days, supported by fast shipping dispatch options through our Dubai trade infrastructure or directly from primary manufacturing facilities.
Yes. We provide complete OEM packaging solutions including 5-ply color retail boxes, customized inner sleeve protection, master shipping carton reinforcement, stack-testing compliance, and pre-printed GTIN/UPC barcode labeling tailored for global distribution networks.
Importers, commercial distributors, and OEM buyers can request samples directly by clicking the Contact Us button on this page. Our engineering team provides immediate consultation, technical drawing reviews, and schedules both virtual or in-person facility audits.
Elevate your commercial culinary portfolio with heavy-duty frying pans and catering hardware engineered for extreme durability, uniform thermal performance, and global compliance.