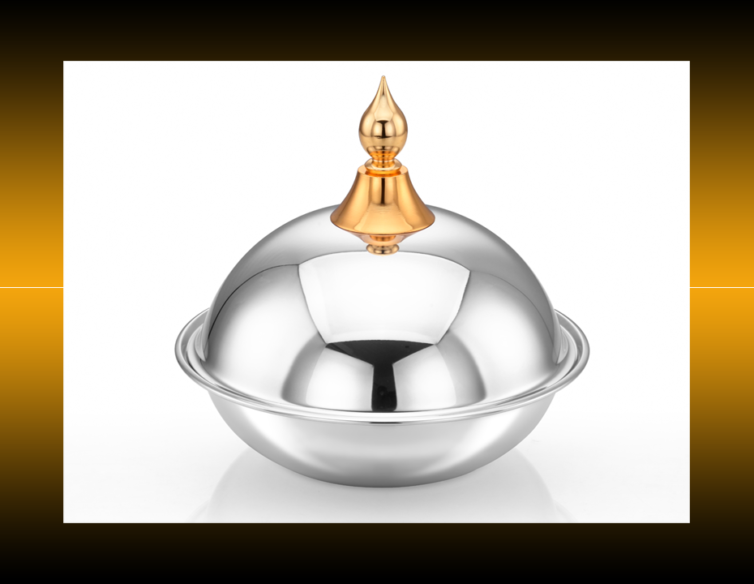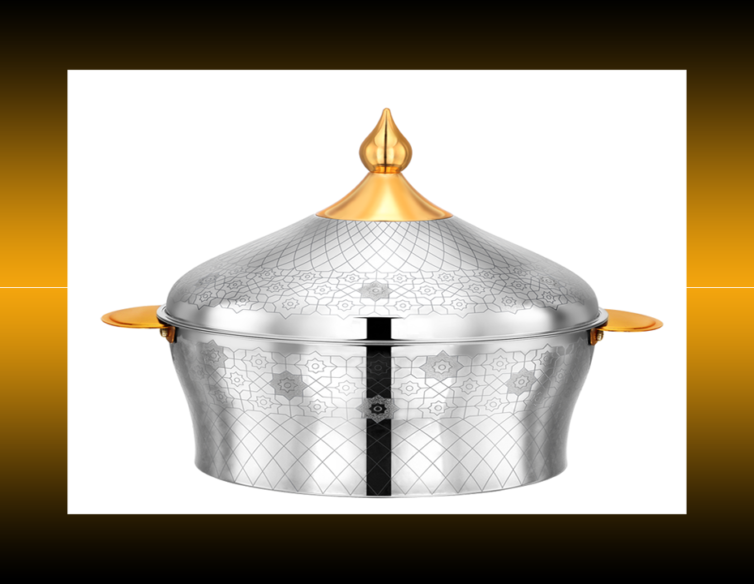
Precision-engineered food-grade stainless steel bowls, insulated thermal casseroles, and commercial heating equipment manufactured in compliance with international FDA, LFGB, and ISO 9001 quality benchmarks.
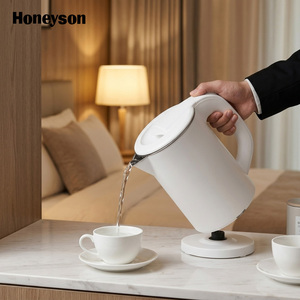
Engineered with a double-wall thermal insulation structure, 304 food-grade stainless steel inner liner, anti-scald outer shell, and rapid boiling element for hotel guestroom and residential use.
Contact Us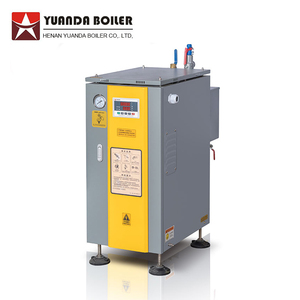
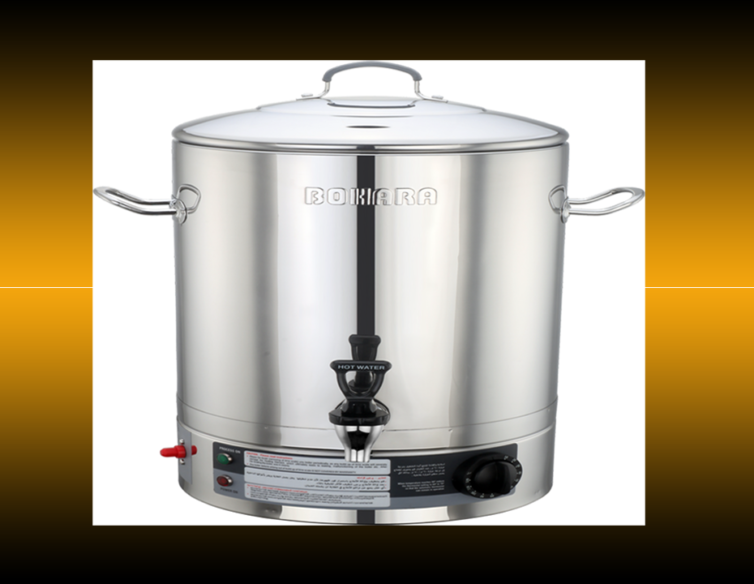
Heavy-duty commercial heating vessel designed for large-scale catering, industrial food processing, and centralized hot water distribution. Features reinforced stainless steel insulation chambers.
Contact Us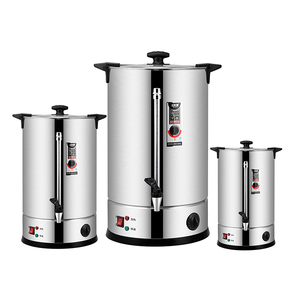
CE-certified high-capacity thermal heating kettle constructed with food-grade 304 stainless steel, double-wall temperature preservation, and precision thermostat control for catering events.
Contact Us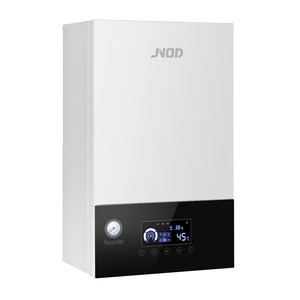
Export-grade OEM electric boiler unit built with dual-circuit thermal exchanger piping and high-density insulation jacket, ideal for commercial kitchens and multi-unit hospitality systems.
Contact Us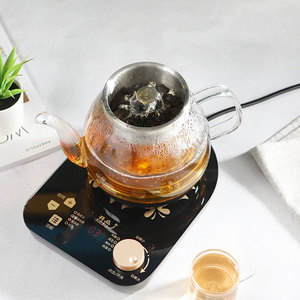
Compact precision boiling pot featuring thermal shock resistant borosilicate glass combined with 304 stainless steel base, removable infusion basket, and digital control module.
Contact Us
Space-saving commercial heating unit featuring double-wall stainless thermal insulation, digital temperature monitoring, and low-energy rapid cycle heating mechanism.
Contact Us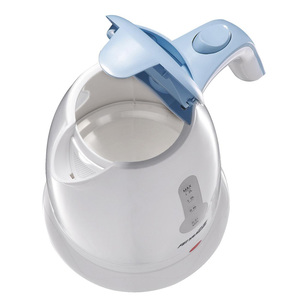
High-grade water heating kettle with food-safe internal lining, dual-layer heat containment housing, transparent water level indicator window, and auto shut-off safety valve.
Contact Us
High-performance vertical electric boiler for restaurant kitchens and commercial establishments. Features twin thermal circuits, double-wall sound dampening, and heavy-duty steel body.
Contact UsAn in-depth analysis of metallurgical grades, thermal insulation physics, deep-drawing manufacturing processes, and quality verification standards for B2B global importers.
Double-wall stainless steel bowls operate on a fundamental thermodynamic principle: conductive heat transfer reduction. By engineering an inner bowl and an outer shell separated by a sealed hollow chamber (either stagnant air gap or evacuated vacuum cavity), thermal transmission between hot food (e.g., soups, noodles, commercial catering dishes) and the exterior environment is reduced by up to 78% compared to single-wall metal tableware.
Furthermore, this double-wall cavity acts as an anti-scald safety barrier. When boiling soup (+95°C) is served, the exterior wall maintains a safe tactile temperature below +42°C, protecting food service staff, restaurant guests, and domestic users from thermal burns while simultaneously eliminating condensation sweating during cold dessert service.
Selecting the correct raw material is the single most crucial factor for OEM procurement officers. Leading Chinese manufacturers utilize specific stainless steel alloys customized for performance requirements:
| Performance Criterion | Commercial Grade (SUS 304 Inner) | Premium Medical/Hospitality (SUS 316) | Economy Grade (SUS 201 Outer / 304 Inner) |
|---|---|---|---|
| Corrosion Resistance | Excellent (Resists organic acids & steam) | Maximum (Resists saline solutions & chlorides) | Moderate (Suitable for standard catering) |
| Thermal Retention Delta | Maintains > 65°C for 2.5 hours | Maintains > 65°C for 4.0 hours (Vacuum insulated) | Maintains > 65°C for 1.5 hours (Air gap) |
| Surface Finishing | Mirror Polish / Satin Brushed | Electropolished / PVD Titanium Plating | Mechanical Satin / Sandblasted |
| Compliance Certification | FDA, LFGB, EU 10/2011, RoHS | FDA, LFGB, NSF Commercial Standard | FDA Standard Compliance |
| Target Application | Hotels, Restaurants, Household Cookware | Luxury Catering, Medical Food Service | Wholesale Supermarkets, Mass Retail |
How evolving global sustainability regulations, smart factory automation in China, and luxury hospitality aesthetic demands are shaping the next decade of double-wall bowl manufacturing.
Environmental ESG regulations in North America and Western Europe are accelerating the demise of traditional chemical electroplating. Leading Chinese factories are investing in physical vapor deposition (PVD) gold, rose gold, and matte black ceramic coatings. PVD provides zero-toxic emission finishes that are scratch-resistant, dishwasher safe, and 100% recyclable.
To mitigate labor inflation, top-tier Chinese double-wall bowl suppliers have implemented fully automated Industry 4.0 production lines. 500-ton hydraulic deep-drawing presses paired with robotic laser welding arms ensure wall thickness uniformity within ±0.02mm, reducing yield defects and enabling high-speed production (up to 30,000 units per shift).
Global container shipping costs have made volumetric freight efficiency a paramount priority. Modern double-wall bowl designs feature engineered taper angles (nestable nesting geometry), allowing bowls to stack compactly without vacuum-locking together. This yields a 35% improvement in shipping carton density, directly lowering landed per-unit transport cost.
The commercial catering sector is increasingly replacing single-layer glass and ceramic serving bowls with insulated double-wall stainless steel hotpots and bowls. Beyond heat retention, commercial buyers prioritize impact durability: stainless steel eliminates breakage risk in high-volume commercial dishwashing environments, drastically reducing lifetime replacement overheads for hotel chains and banquet operators.
Building upon five decades of foundational excellence since 1974, our manufacturing group (incorporating the heritage of BOHARA Group) represents the pinnacle of Chinese and international metalware production. We combine traditional metallurgical craftsmanship with state-of-the-art automated manufacturing infrastructure.
Essential technical answers regarding MOQ, custom OEM branding, quality control procedures, thermal insulation testing, and customs compliance for global importers.
Air-insulated double wall bowls contain trapped ambient air inside the hermetically sealed cavity between the inner and outer stainless steel walls. This provides excellent anti-scald protection and moderate heat retention (1 to 2 hours). Vacuum-insulated bowls undergo a high-temperature vacuum furnace process to evacuate air from the cavity, completely removing conductive gas molecules. Vacuum insulation maintains serving temperatures above 65°C for 4 to 6 hours, making it ideal for premium thermal lunchware and commercial catering carriers.
Authentic Grade 304 stainless steel contains a minimum of 18% Chromium and 8% Nickel. Importers can verify material authenticity through three primary methods: 1) Chemical Spectrometer (XRF) Testing on-site during inspection; 2) Requesting Mill Test Certificates (MTC) matching the heat lot number of the steel coil; and 3) Acid Drop Test Reagents (SUS304 turns light green or remains clear, while SUS201 turns red within seconds due to low nickel content).
China top suppliers provide end-to-end OEM/ODM customization: laser-etched or stamped bottom logos, custom color PVD titanium plating, matte powder coating, custom surface textures (hammered, brushed, satin, or mirror finish), customized box packaging (color gift boxes, mail-order drop-test packaging), and custom volumetric capacities (from 250ml tasting bowls up to 5000ml commercial serving basins).
Yes, provided the bowl features a fully continuous, 360-degree automated laser-welded rim seam. High-quality double-wall bowls manufactured in top Chinese facilities undergo pressure-immersion leak testing to ensure water vapor cannot enter the internal air cavity during high-pressure commercial dishwashing cycles (85°C rinse water).
Standard MOQs for custom logo/color double-wall bowls range from 1,000 to 3,000 units per size for standard catalog items, and 5,000 units for completely customized die-cut shapes. Production lead times average 25 to 35 days post-sample approval, while prototype 3D/die samples are typically delivered within 7 to 10 working days.
Reputable suppliers hold ISO 9001:2015 quality management certification and provide product-level testing compliance with FDA 21 CFR (United States), LFGB (Germany), EU Regulation 1935/2004, DGCCRF (France), and NSF International standards for commercial kitchen sanitation.
Export products are packed using multi-layer protective protocols: 1) Individual OPP bio-degradable polybags; 2) Interlocking tissue wrap or bubble sleeves; 3) Heavy-duty 5-ply corrugated dividers within inner boxes; and 4) Reinforced 7-ply export master cartons strapped on wooden or plastic pallets for container sea freight.
Direct factory procurement offers a 20% to 35% cost margin reduction, direct access to in-house metallurgical engineers for rapid product modification, complete control over raw material specifications, and priority production scheduling for seasonal retail rollouts.
Streamline your supply chain with direct factory pricing, certified food-grade materials, and OEM custom tooling solutions tailored to your business needs.